ISO 9001:2015 CERTIFIED (No. 29024010637-03R0S) Shenzhen Factory: ONLINE (2h Rapid DFM Response Guarantee)
ALUMINUM ALLOYS • VOLUME DIE CASTING

Cast Aluminum A380 & ADC12 Die Casting Alloys

Optimal Fluidity, Pressure Tightness, and Dimensional Stability for High-Volume Castings.

A380 (US standard) and ADC12 (Japanese JIS standard) are the premier silicon-copper-aluminum alloys for high-pressure die casting. Featuring excellent liquid melt fluidity, hot tear resistance, and high stiffness, these alloys excel in thin-walled automotive transmission housings, LED lighting heat-sink bodies, and electric tool enclosures produced in quantities from 500 to 500,000 pieces.

Thin Walls down to 1.5mm
High Thermal Conductivity
ISO 9001 & IATF 16949

Material Engineering for Cast Aluminum A380 & ADC12 Die Casting Alloys

Certified raw material sourcing, certified heat-treatment verification, and extreme tolerance manufacturing calibrated specifically for Cast Aluminum A380 & ADC12 Die Casting Alloys components.

High Melt Fluidity

8.5-12.0% silicon content ensures complete mold cavity filling of deep cooling fins and complex geometries.

Post-Cast CNC Machining

In-house 4-axis CNC machining of bearing bores, O-ring seal grooves, and tapped holes down to ±0.01mm.

X-Ray Porosity Inspection

Real-time digital X-ray radiography inspection ensures zero critical gas porosity along high-pressure oil paths.

Superior Thermal Dissipation

Thermal conductivity of 96-113 W/m-K provides high-efficiency passive cooling for 5G telecommunication boxes.

Technical Deep Dives & Processing Notes

Detailed manufacturing insights covering tooling kinematics, thermal management, surface finishing, and dimensional inspection for Cast Aluminum A380 & ADC12 Die Casting Alloys.

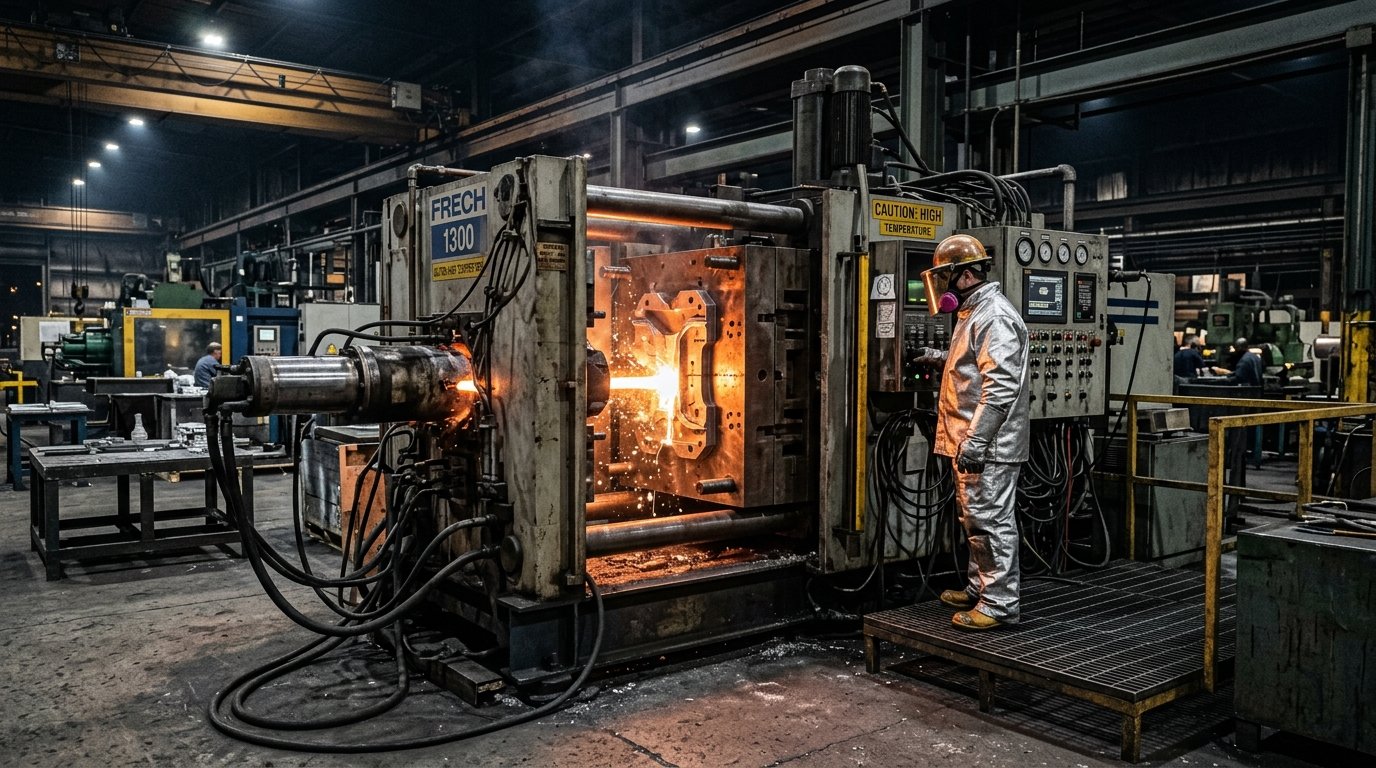
Multi-Slide High-Pressure Die Casting (280T to 1600T Machines) 500 × 500 HD

Multi-Slide High-Pressure Die Casting (280T to 1600T Machines)

Automated cold-chamber die casting machines equipped with robot ladlers and spray systems produce high-integrity A380 gearboxes with cycle times under 45 seconds.

  • Machined with calibrated multi-axis kinematics minimizing tool deflection
  • GD&T true position inspected within ±0.005mm using automated CMM
  • Full material mill certs, heat treat data, and FAI documentation provided
Request Quotation for Similar Geometry
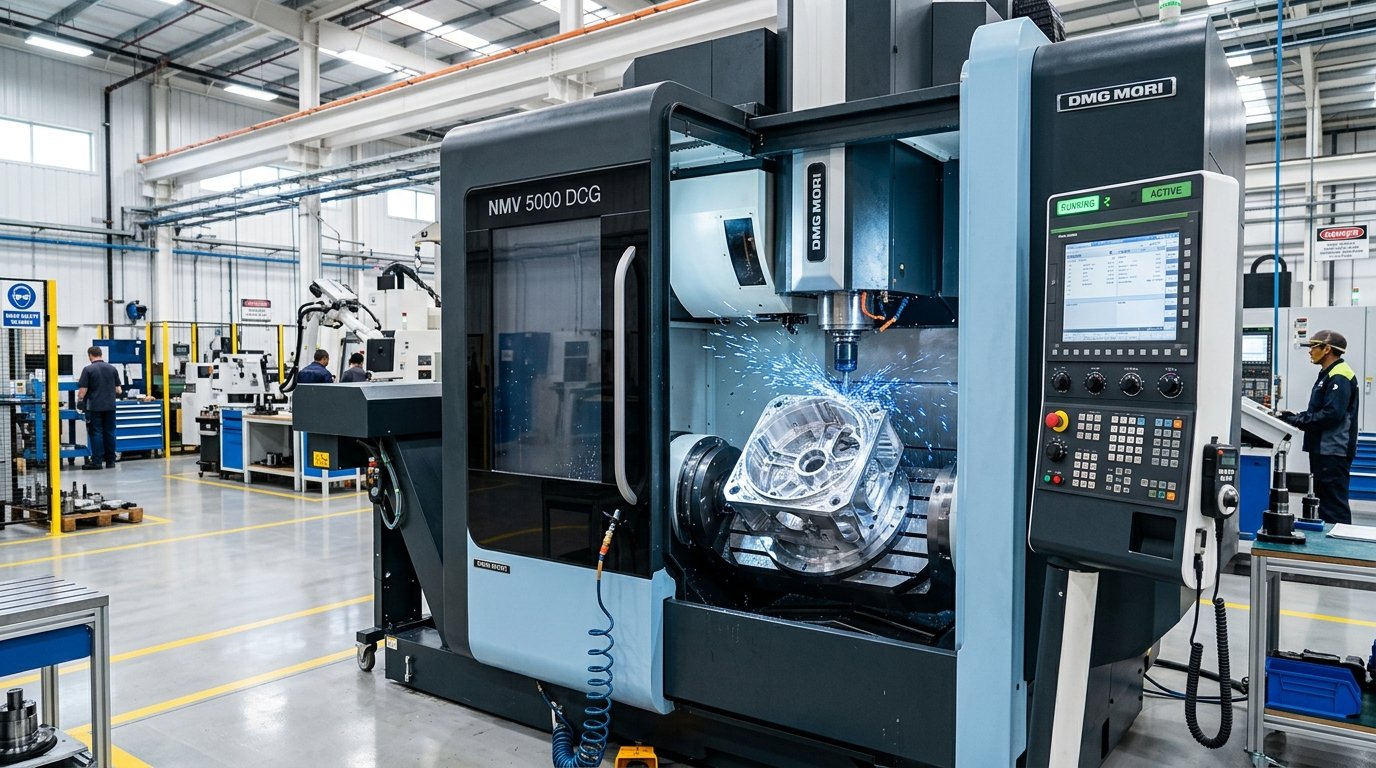
Precision Secondary CNC Machining on Cast Housings 500 × 500 HD

Precision Secondary CNC Machining on Cast Housings

Custom hydraulic clamping fixtures secure raw castings for finish milling of gasket mating faces, precision bearing journals, and M3-M12 helical thread tapping.

  • Machined with calibrated multi-axis kinematics minimizing tool deflection
  • GD&T true position inspected within ±0.005mm using automated CMM
  • Full material mill certs, heat treat data, and FAI documentation provided
Request Quotation for Similar Geometry
Shot Blasting, E-Coating & Durable Powder Painting 500 × 500 HD

Shot Blasting, E-Coating & Durable Powder Painting

Stainless steel shot blasting cleans casting flash and part parting lines, creating an anchor profile for thermoset epoxy powder coating with 500+ hours salt spray durability.

  • Machined with calibrated multi-axis kinematics minimizing tool deflection
  • GD&T true position inspected within ±0.005mm using automated CMM
  • Full material mill certs, heat treat data, and FAI documentation provided
Request Quotation for Similar Geometry
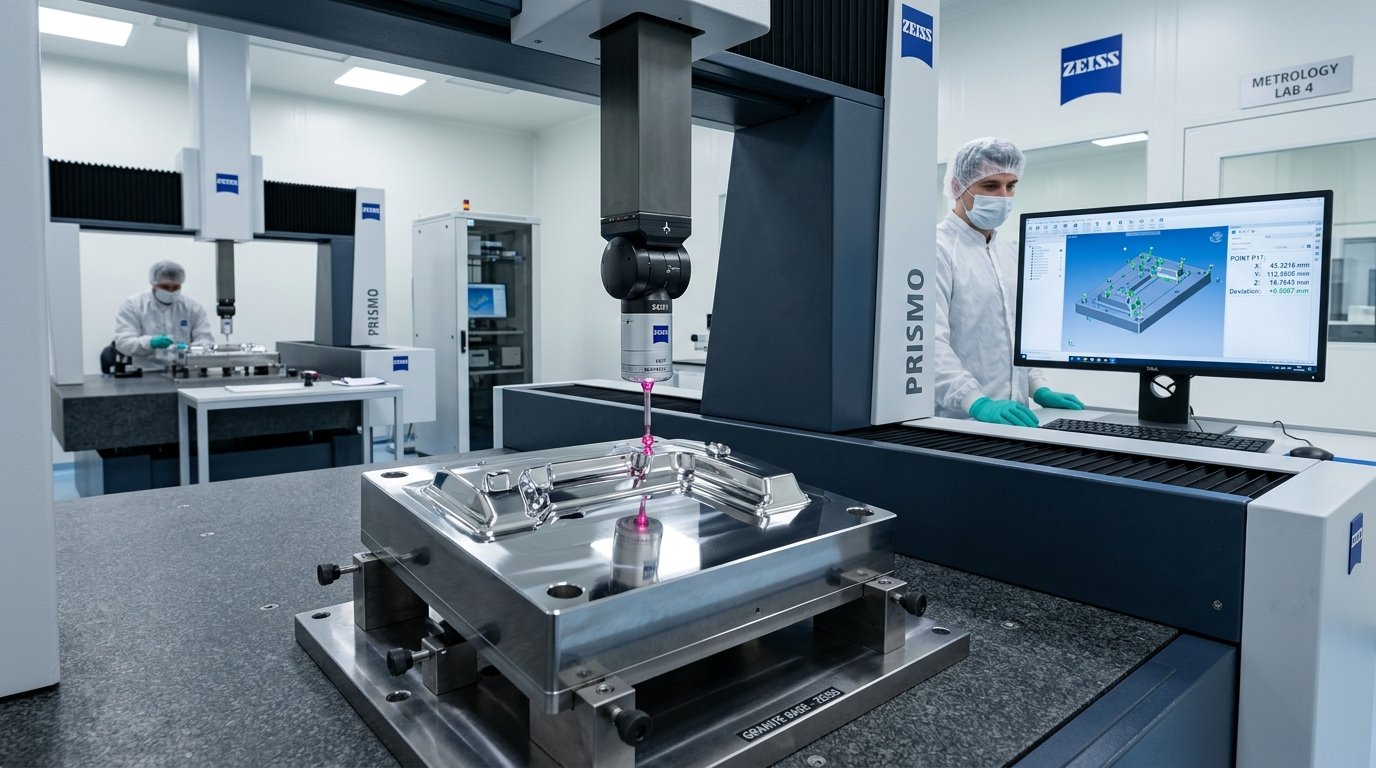
Helium Leak Testing & 3D CMM Geometric Metrology 500 × 500 HD

Helium Leak Testing & 3D CMM Geometric Metrology

Pressure-tight oil pumps and fluid manifolds undergo 100% differential air-pressure decay testing to guarantee zero micro-porosity leakage under 10 bar operating pressure.

  • Machined with calibrated multi-axis kinematics minimizing tool deflection
  • GD&T true position inspected within ±0.005mm using automated CMM
  • Full material mill certs, heat treat data, and FAI documentation provided
Request Quotation for Similar Geometry

Capabilities & Quality Protocols

Every part manufactured from Cast Aluminum A380 & ADC12 Die Casting Alloys adheres to international metallurgy standards and rigorous metrology protocols.

Material Specifications & Properties

  • A380 Composition: 7.5-9.5% Si, 3.0-4.0% Cu, 0.1% Mg, max 1.3% Fe, bal Al
  • ADC12 Composition: 9.6-12.0% Si, 1.5-3.5% Cu, 0.3% Mg, bal Al
  • Tensile: 324 MPa (A380) / 310 MPa (ADC12) | Yield: 160 MPa | Hardness: 80-85 HB
  • Shot weight range: 50 grams to 15 kg on cold chamber machines up to 1600 tons

Metrology & Quality Assurance

  • Zeiss PRISMO 3D CMM Metrology with scanning resolution down to 0.9µm
  • Keyence Optical Non-Contact Flash Measuring System for micro-features
  • XRF Spectrometry for raw metal alloy composition verification
  • AS9102 Form 1, Form 2, and Form 3 First Article Inspection (FAI) packages

Ready to Prototype or Scale Cast Aluminum A380 & ADC12 Die Casting Alloys?

Upload your 3D CAD models (.STEP, .IGES, .SLDPRT, .X_T) or 2D technical drawings (.PDF, .DWG) to receive an interactive quote with comprehensive Design for Manufacturability (DFM) feedback in under 2 hours.

Upload CAD Files Now

Frequently Asked Questions

Common engineering questions regarding tolerances, material traceability, and turnaround for Cast Aluminum A380 & ADC12 Die Casting Alloys.

What is the main difference between A380 and ADC12? +
ADC12 has higher silicon content (up to 12%), giving it slightly better fluidity for very intricate or thin-walled parts, while A380 is the North American standard equivalent.
What minimum wall thickness can you die cast in A380? +
Standard minimum wall thickness is 1.5mm to 2.0mm. In localized areas with optimal gate placement, wall thicknesses of 1.2mm can be achieved.
Can A380 castings be anodized? +
High silicon and copper contents cause standard clear anodizing to turn a dark mottled grey. For cosmetic finishes, we recommend shot blasting, e-coating, or powder coating.
What is the typical tooling lifespan for aluminum die cast molds? +
Made from premium H13 or DIEVAR hot-work tool steel, our die casting molds reliably produce 80,000 to 120,000 shots before cavity replacement is required.
💬

Connect on WeChat

Scan the QR code or search WeChat ID to speak directly with our Shenzhen engineering team.

WeChat ID: JYH-Prototype
JYH AI Assistant · 智能客服
Online 24/7 · 全天在线
Get Instant Quote
Shenzhen High-Tech Industrial Park
+86 137 1457 8126