ISO 9001:2015 CERTIFIED (No. 29024010637-03R0S) Shenzhen Factory: ONLINE (2h Rapid DFM Response Guarantee)
Home / Divisions / Manufacturing Divisions
CORE DIVISION 06

Vacuum Casting & Wire EDM Division

Polyurethane Silicone Mold Casting & Sub-Micron Wire Electrical Discharge Machining.

The Vacuum Casting & Wire EDM Division combines low-cost short-run polyurethane molding with ultra-hard micro-precision metal machining. Using soft silicone tooling, we replicate 10 to 100 functional plastic parts with molded-in color and texture. Concurrently, our slow-feed Wire EDM cells machine hardened tool steels and tungsten carbide with sub-micron accuracy.

10 to 100 Parts per Silicone Mold
Wire EDM Precision: ±0.003mm
Molded Colors & Textures

Built for Precision, Scalability and Speed

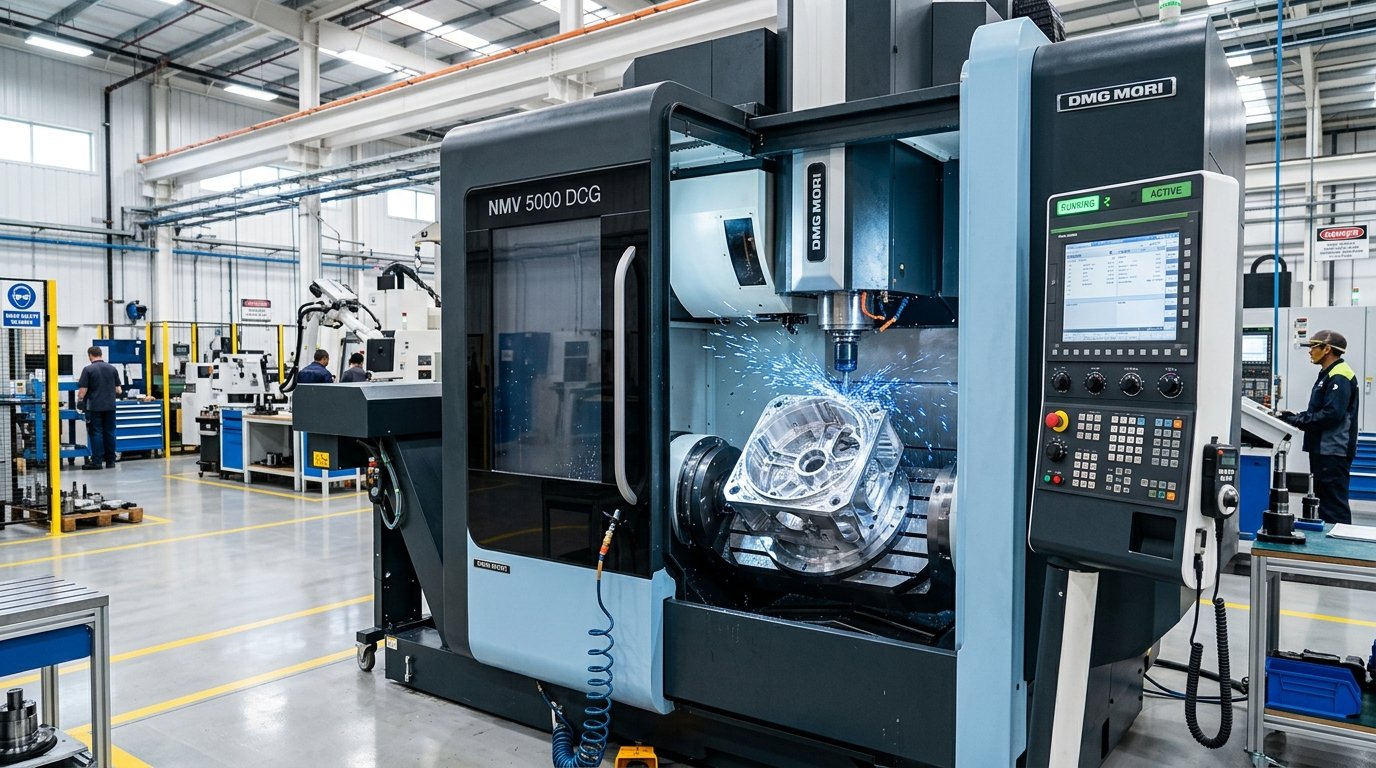
Shenzhen Jinyihe Technology combines advanced multi-axis CNC machines, certified metrology, and deep production expertise to bring high-complexity parts to market with zero delays.

Silicone Tooling Casting

Low-cost polyurethane casting mimicking ABS, PC, POM, and rubber with molded textures.

Sub-Micron Wire EDM

Slow-feed brass wire erosion cutting hardened tool steel up to 60 HRC with ±0.003mm accuracy.

Sharp Internal Radii

Wire cutting internal square corners down to R 0.05mm impossible for rotating rotary endmills.

Color Matching & Clear Optics

Custom Pantone pigments and optical water-clear polyurethane resins for lenses and light pipes.

In-Depth Manufacturing Analysis

Discover how our advanced machinery, certified cleanroom facilities, and strict quality control protocols ensure reliable execution for mission-critical hardware.

ARTICLE 01 Polyurethane Vacuum Casting in Silicone Tooling

Polyurethane Vacuum Casting in Silicone Tooling

The Most Cost-Effective Method for 10 to 100 Functional Plastic Parts

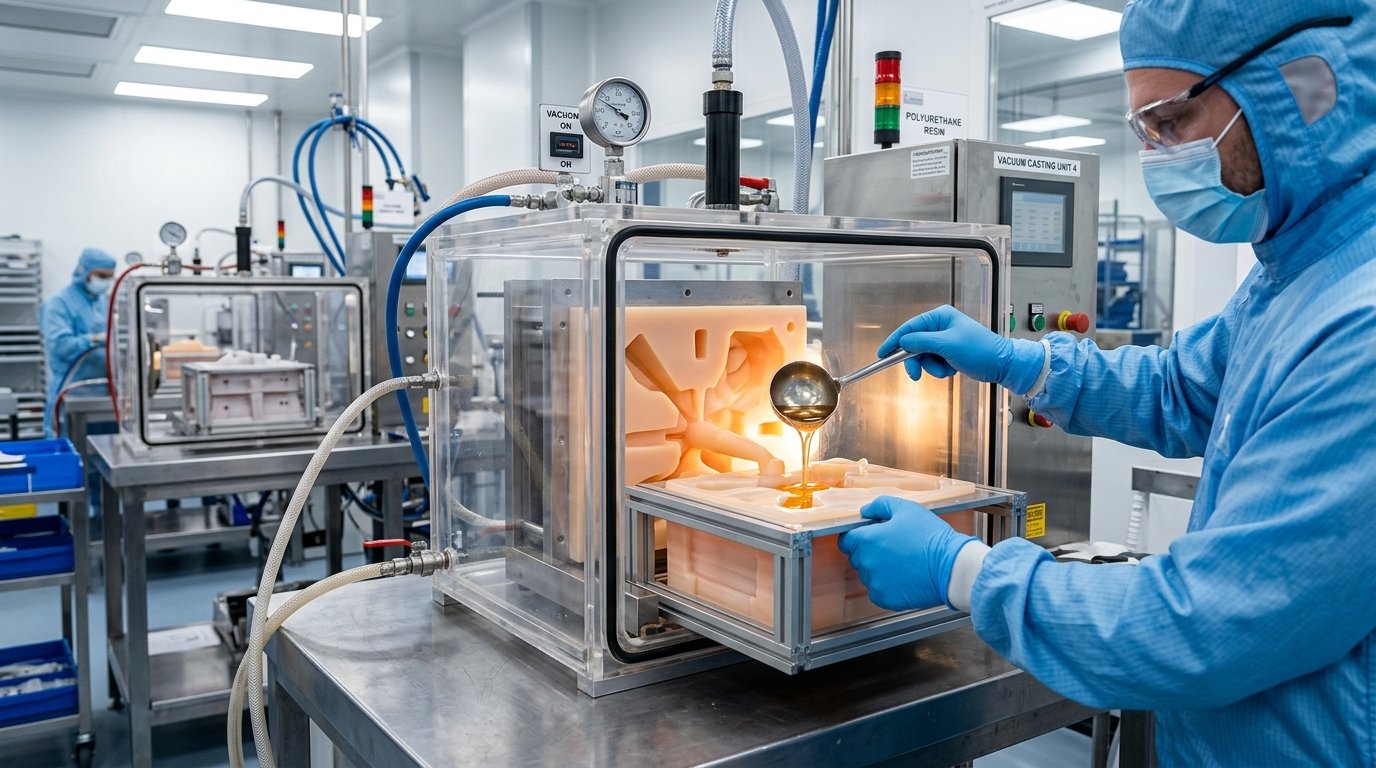
When you need 20 to 50 plastic parts for field trials, trade shows, or early customer shipments, hard steel tooling is too expensive and 3D printing is too slow. Vacuum casting solves this by using a high-resolution SLA master pattern to cast a room-temperature vulcanizing (RTV) silicone rubber mold. In a vacuum de-airing chamber, two-part polyurethane resins are injected, producing bubble-free parts with injection-molded appearance.

Key Engineering Takeaways
  • Molds produced in just 3 to 5 business days without expensive CNC metal tooling
  • Polyurethane resins engineered to replicate ABS, Polycarbonate, Polypropylene, and soft Rubber
  • Molded-in custom color pigments eliminating secondary paint chipping risks
ARTICLE 02 Slow-Feed Wire EDM for Ultra-Hard Conductive Metals

Slow-Feed Wire EDM for Ultra-Hard Conductive Metals

Sub-Micron Spark Erosion with Zero Tool Contact Force

Machining hardened tool steels (D2, H13, 60 HRC), titanium, and sintered carbides destroys traditional carbide milling cutters. Our slow-feeding Wire Electrical Discharge Machines (EDM) use an electrically charged micro-brass wire submerged in deionized dielectric fluid. By creating millions of microscopic electrical sparks per second, the metal is vaporized without mechanical contact or cutting stresses.

Key Engineering Takeaways
  • Micro-precision tolerances held down to ±0.003mm across tall workpiece heights up to 350mm
  • Zero mechanical cutting force prevents distortion on fragile, ultra-thin metal fins
  • Mirror-like surface finish directly off the wire down to Ra 0.2μm
ARTICLE 03 Sinker EDM (Ram EDM) for Deep Cavities & Blind Features

Sinker EDM (Ram EDM) for Deep Cavities & Blind Features

Forming Complex Geometric Cavities in Hardened Injection Mold Dies

For deep, sharp-cornered blind cavities in steel injection molds where wire EDM cannot pass through, our division deploys CNC Sinker EDM. We machine custom graphite or copper electrodes on high-speed CNC mills, then spark-erode the inverse geometry into hardened mold cavities with multi-axis orbital motion.

Key Engineering Takeaways
  • Ultra-sharp internal 90° corners with radii down to 0.02mm for mold shutoffs and ribs
  • Mirror-finish sparking settings eliminating hand-polishing on optical mold cores
  • Machining blind keyways, splines, and micro-slots in pre-hardened aerospace alloys
ARTICLE 04 Optical Clear Resin & Overmolded Elastomeric Parts

Optical Clear Resin & Overmolded Elastomeric Parts

Water-Clear Polyurethane Lenses and Multi-Durometer Functional Seals

Vacuum casting excels at optical transparency and elastomeric durometer control. We cast water-clear polyurethanes with high UV stability that will not yellow over time, ideal for automotive headlight prototypes and medical fluidic viewing chambers. We also cast multi-durometer parts, combining rigid polyurethane cores with soft rubber gaskets in a single demolding.

Key Engineering Takeaways
  • High optical transparency (92% light transmission) mimicking molded polycarbonate and PMMA
  • Elastomeric durometers ranging from soft Shore 30A to rigid Shore 90D
  • Overmolded threaded brass inserts and metal pins locked securely into cast urethane

Vacuum Casting & EDM Division Capabilities

Official engineering tolerances, machinery specifications, and production thresholds maintained at our Shenzhen plant.

Technology Typical Batch Size Achievable Tolerance Key Materials
Polyurethane Vacuum Casting 10 to 100 Parts per Mold ±0.15 mm per 100 mm ABS-like, PC-like, PP-like, Shore 30A-90A Urethane
Slow-Feed Wire EDM 1 to 500+ Precision Parts ±0.003 mm (0.0001 in) Hardened Tool Steels (H13, D2), Titanium, Carbides
CNC Sinker / Ram EDM Tooling Dies & Blind Pockets ±0.005 mm (0.0002 in) Copper/Graphite Electrodes into Hardened Steels
Optical Clear Urethane Casting 10 to 50 Optical Units ±0.20 mm (Uniform) High-transparency UV-stabilized PU Resin

Ready to Start Your Next Production Run?

Upload your 3D CAD files (.STEP, .STP, .IGES) today for an automated Design for Manufacturability (DFM) review and direct factory pricing.

Frequently Asked Questions

Direct answers regarding our manufacturing lead times, tolerances, certified materials, and global delivery.

Vacuum casting is ideal for low-volume runs of 10 to 100 parts where you need the look, feel, and mechanical properties of injection molded plastic without high tooling costs.
A silicone mold typically produces 15 to 25 parts before the mold details begin to degrade. For runs of 50 to 100 parts, we cast multiple silicone tools from the same master.
Wire EDM uses an electrically charged brass wire to cut conductive metals via spark erosion. It is used for ultra-hard metals (up to 60 HRC), tall vertical cuts, and sharp internal corners.
Yes. We blend custom color pigments directly into the liquid polyurethane resin before casting, providing consistent color throughout the part with no chipping.
💬

Connect on WeChat

Scan the QR code or search WeChat ID to speak directly with our Shenzhen engineering team.

WeChat ID: JYH-Prototype
JYH AI Assistant · 智能客服
Online 24/7 · 全天在线
Get Instant Quote
Shenzhen High-Tech Industrial Park
+86 137 1457 8126